


High-Carbon Gold Ore Carbon-in-Pulp Processing Plant: Complete Set of Equipment and Analytical Electrolysis Solution
High-Carbon Gold Ore Carbon-in-Pulp (CIP) Processing Plant: Complete Set of Equipment and Electrolytic Leaching Solution
High-carbon gold ore is widely recognized as a “tough nut to crack” in gold ore beneficiation.The carbonaceous materials in this type of ore (graphite, activated carbon, humic acid, etc.) possess adsorption properties similar to those of activated carbon, causing gold cyanide complexes that have already dissolved into the solution to be re-adsorbed back onto the solid phase, resulting in a situation where “leaching is possible, but recovery is not.”Conventional cyanide leaching recovery rates typically range from only 20–50%, while reagent consumption remains high. Many mine owners have built carbon-in-pulp plants with high-quality equipment and well-established processes, yet recovery rates still fail to improve—the problem often lies not in the leaching tanks, but in the failure to effectively treat the carbonaceous materials prior to leaching.
This article focuses on the construction of carbon-in-pulp processing plants for high-carbon gold ore. Covering topics ranging from gold entrapment mechanisms, pretreatment pathways, and CIP/CIL process selection to the configuration of a complete set of mechanical equipment and electrolysis solutions for desorbing gold-bearing carbon,systematically outlining a practical technical roadmap to help investors in high-carbon gold ore projects build processing plants correctly, select the right equipment, and boost recovery rates.
I. Understanding “Gold Trapping”: Why High-Carbon Gold Ore Is Difficult to Process
The design of a mineral processing plan must start with the characteristics of the ore. The difficulty in processing high-carbon gold ore stems primarily from four aspects:
1. Carbonaceous matter acts as “natural activated carbon.” The surface of carbonaceous matter in the ore possesses a large number of active adsorption sites, with adsorption properties similar to those of activated carbon.During cyanide leaching, gold is dissolved into the solution as gold cyanide complexes; however, the carbonaceous material “re-captures” this dissolved gold back into the solid phase, much like activated carbon adsorbs gold. The result is that while the gold is leached out, it cannot be recovered, leading to abnormally high grades in the tailings.
2. The type of carbonaceous material determines its gold-snatching capacity. Activated carbon has the strongest adsorption capacity, followed by graphite, while humic acid-type materials are relatively weaker.The higher the carbon content and the greater the activity, the more severe the gold-snatching effect becomes, and the greater the need for pretreatment. This is also why, among ores all classified as “carbon-bearing ores,” some achieve leaching rates of over 90% after pretreatment, while others consistently remain at low levels.
3. They often occur in association with arsenic and sulfur, compounding the challenges of processing. High-carbon gold ores frequently occur alongside arsenopyrite, arsenic trioxide, and other arsenic-bearing minerals. Arsenic encapsulates the gold within sulfides, making it impossible to extract no matter how finely the ore is ground; carbon, in turn, reabsorbs the dissolved gold.Under these dual interferences, conventional cyanide leaching yields pitifully low recovery rates, with reagents entirely wasted on ineffective reactions.
4. Direct leaching is not economically viable. Direct cyanidation without pretreatment not only results in low leaching rates but also high cyanide consumption, making it extremely uneconomical.High-carbon gold ores must have their carbonaceous material “passivated” or removed prior to leaching to eliminate the gold-sequestration effect; only then can subsequent cyanide recovery rates return to normal levels.
To sum it up in one sentence: High-carbon gold ore is difficult to process—not because the gold is hard to leach, but because the leached gold is “stolen” by carbonaceous material. The top priority in designing a carbon-in-pulp plant is pre-treatment before leaching, not the number of leaching tanks.
II. How to Choose a Pretreatment Pathway: Eliminate the Gold-Snatching Effect First
To address the gold-stealing effect of carbonaceous material, the industry primarily employs the following pre-treatment approaches. The choice depends on the content, type, and occurrence state of the carbonaceous material and must be verified through comparative mineral processing tests:
1. Suppressing carbon-bearing materials via flotation. Add carbon-bearing material inhibitors during the flotation stage to prevent these materials from floating to the surface, thereby avoiding their enrichment in the concentrate or interference with the flotation foam; or employ priority flotation, first floating out the carbon-bearing materials before floating the gold sulfides.Another function of flotation is to concentrate gold-bearing sulfides into concentrate, thereby reducing the volume of material requiring subsequent cyanidation—by processing only the concentrate rather than the entire ore stream, the scale of both leaching tanks and adsorption systems can be scaled down.
2. Chlorination/chemical oxidation pretreatment. Oxidative passivation of carbonaceous material is achieved using chlorinating agents (such as sodium hypochlorite or chlorine) or other oxidizing agents to destroy its surface-active adsorption sites, thereby eliminating the material\'s ability to adsorb gold cyanide complexes.This is one of the mainstream pre-treatment methods for high-carbon gold ores. The key lies in controlling chemical dosage and reaction conditions to passivate carbonaceous materials while avoiding excessive oxidation that could adversely affect subsequent leaching.
3. Roasting pretreatment. High-temperature roasting and oxidation remove carbonaceous matter and sulfides, eliminating the gold-kidnapping effect and breaking open sulfide capsules. This method is thorough but involves high energy consumption and environmental protection costs; it is suitable for ores with high carbon content where other methods are ineffective.
4. Bio-oxidation/Pressurized Oxidation Pretreatment. Biological oxidation utilizes microorganisms to oxidize and decompose sulfides; it is relatively low-cost and environmentally friendly, but the process takes a long time. Pressurized oxidation oxidizes sulfides and carbonaceous matter under high temperature and pressure; it is highly effective and fast, but involves higher equipment investment and operating costs, making it suitable for large-scale projects and highly refractory ores.
Key Consideration: No single pretreatment method is a one-size-fits-all solution.The selection of a pretreatment method for carbonaceous gold ores depends on the carbon, arsenic, and antimony content and their occurrence conditions. It must be verified through comparative mineral processing tests, and the economic trade-off between the increase in leaching efficiency and pretreatment costs must be carefully calculated. If, after diagnosis, it is confirmed that the project has no economic value, this should be honestly communicated; blind sales pitches should be avoided.
III. How to Choose a Carbon-in-Pulp Process: CIP or CIL
Once pre-treatment has resolved the issue of gold loss, the next step is to recover the dissolved gold. The primary processes for this step are cyanide leaching combined with activated carbon adsorption, namely CIP (Carbon-in-Pulp) and CIL (Carbon-in-Leach).
CIP (Carbon-in-Pulp): Leaching precedes adsorption, allowing for more precise control. Leaching is completed first; activated carbon is added after the ore slurry enters the adsorption tank. Leaching and adsorption occur in separate tanks, allowing for a more thorough leaching period. This method is suitable for ores with relatively fast leaching rates that require staged control and is commonly used in large-scale processing plants.For high-carbon gold ores, since sufficient leaching time must still be ensured after pretreatment, the advantages of CIP\'s staged control are even more pronounced—the leaching stage allows for independent optimization of time, while the adsorption stage enables independent control of carbon concentration.
CIL (Carbon-in-Leach): Leaching and adsorption occur simultaneously, resulting in a compact process. Leaching and activated carbon adsorption take place concurrently in the same leaching tank; activated carbon is added at the end of the tank and moves forward in a countercurrent flow.The advantages include fewer tanks, a compact process, and relatively low capital investment, making it suitable for small- to medium-sized as well as large processing plants. If the gold-stripping effect has been completely eliminated after pretreatment and the ore leaches relatively quickly, the compact CIL process offers greater economic efficiency.
Selection Criteria: When selecting a carbon-in-leach process for high-carbon gold ores, one must not focus solely on capital investment but must also consider the effectiveness of pretreatment and leaching kinetics.For ores where carbon-bearing materials are thoroughly passivated after pretreatment and leaching rates are fast, the compact CIL process is cost-effective; for ores where residual interferents remain after pretreatment and leaching rates are slow, the CIP process—which involves leaching followed by absorption—is a more reliable choice. The specific selection should be validated through leaching tests and comparative CIP/CIL tests, rather than decided on a whim.
IV. Complete Mechanical Equipment Configuration: From Crushing to Concentrated Gold
The complete set of equipment for a carbon-in-slurry (CIL) processing plant for high-carbon gold ore is organized by process stage as follows:
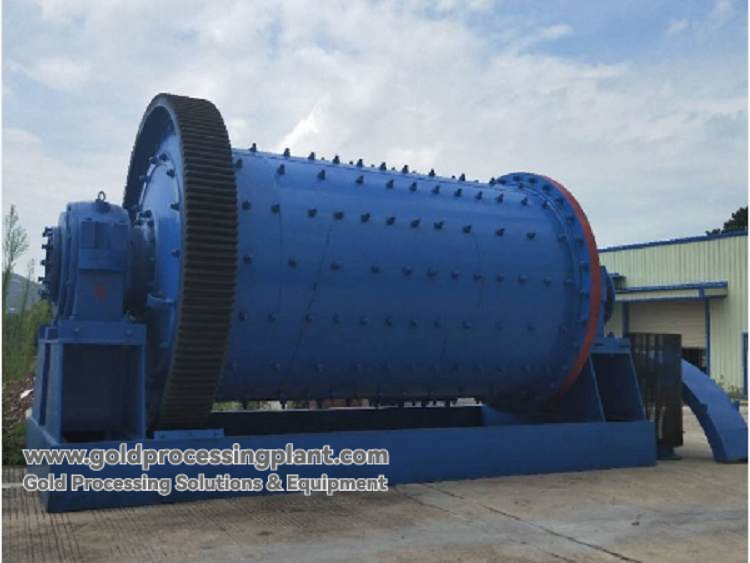
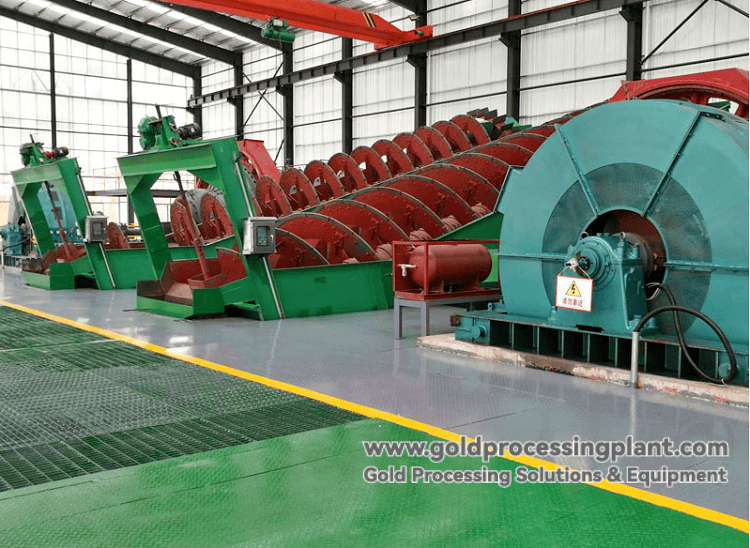
Crushing and Grinding Section: Jaw crusher (primary crushing; handles large chunks of raw ore; simple structure and durable) + Cone crusher (secondary and fine crushing; highly efficient at processing hard rock; uniform product size)+ Ball Mill (two-stage grinding: grid type + overflow type) + Spiral Classifier/Hydrocyclone (closed-circuit classification). The grinding fineness must ensure the individual liberation of gold-bearing minerals while avoiding over-grinding. The crushing stage follows the principle of “crush more, grind less” to reduce energy consumption during grinding.
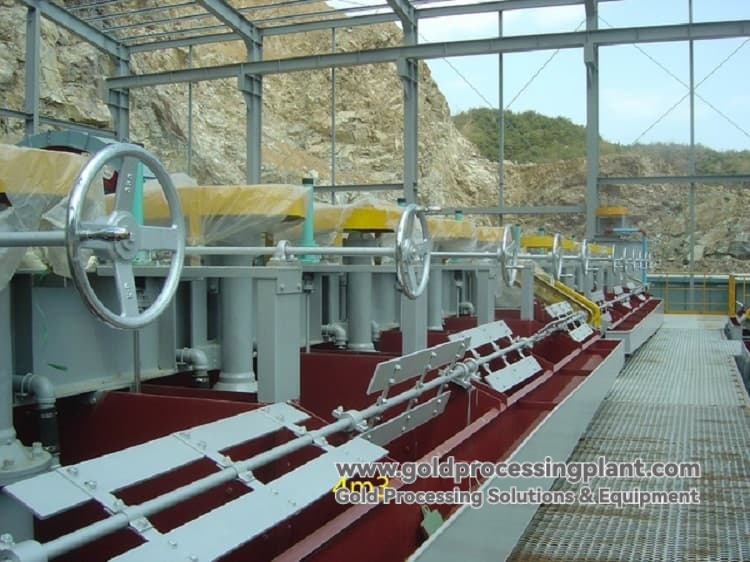
Flotation Section (if flotation pretreatment is used): Flotation machine series (SF-type self-suction pulp, suitable for the front end of roughing and scavenging; XCF/KYF-type aerated, the preferred choice for large-scale direct-flow cell configurations), combined roughing, scavenging, and concentrating units;Supporting agitation tanks and dosing systems (including carbonaceous material inhibitor addition).
Pre-treatment Section: Pre-treatment reaction tanks (with agitation and corrosion-resistant linings), chlorinating agent/oxidizing agent dosing units, pH adjustment systems, and ventilation and exhaust gas treatment units.Equipment materials must be upgraded with corrosion protection specifically designed for the corrosive chloride/oxidizing environment (corrosion-resistant stainless steel or internally lined with a corrosion-resistant coating)—selecting the wrong materials will significantly shorten the equipment\'s service life.
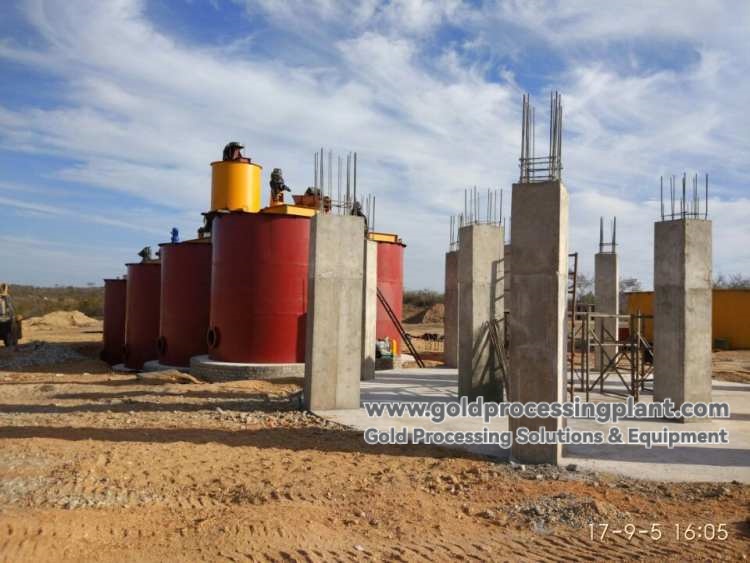
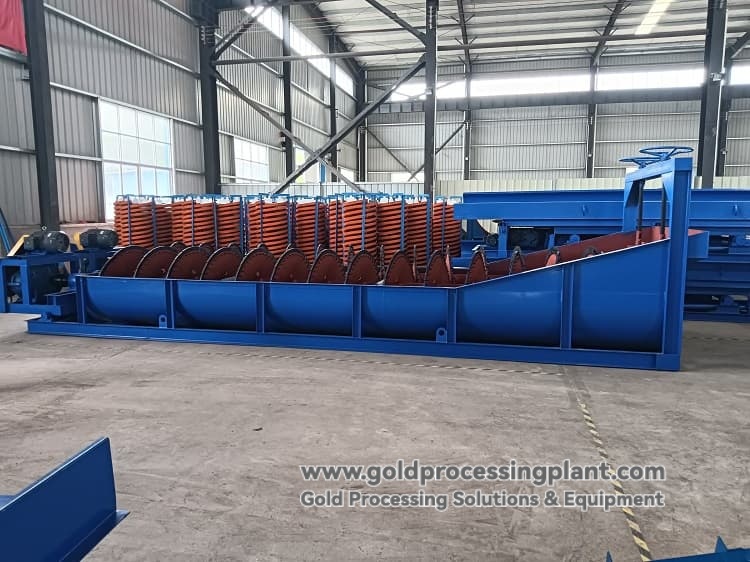
Leaching and Adsorption Section (CIP/CIL): Leaching tanks (with agitation and aeration, multiple tanks in series), activated carbon adsorption system, gold-bearing carbon separation screen (carbon separator/air lifter), and carbon lifter.The carbon-retaining screen prevents activated carbon from being carried away with the slurry, while the carbon extractor lifts and extracts the gold-loaded carbon from the tank; these specific pieces of equipment directly affect carbon consumption and recovery rates. The CIL process also requires a high-efficiency dual-impeller carbon leaching tank.
Desorption and Electrolysis Section (Core Equipment): After acid washing, the gold-loaded carbon enters the desorption and electrolysis system, where the gold is eluted and electrolytically converted into gold slime. Equipment includes desorption columns, electrolytic cells, rectifier power supplies, heating systems, acid washing tanks, and storage tanks.Desorption and electrolysis equipment operating at ambient temperature and pressure is suitable for routine processing, with lower capital and operating costs; high-temperature, high-pressure desorption and electrolysis equipment offers higher processing efficiency and more thorough desorption, making it suitable for large-scale mines or ores that are difficult to desorb. Equipment selection must be based on the gold content of the gold-bearing carbon, processing capacity, and target desorption rate.
Smelting Section: The gold slurry is smelted in a gold smelter to produce high-purity gold ingots.
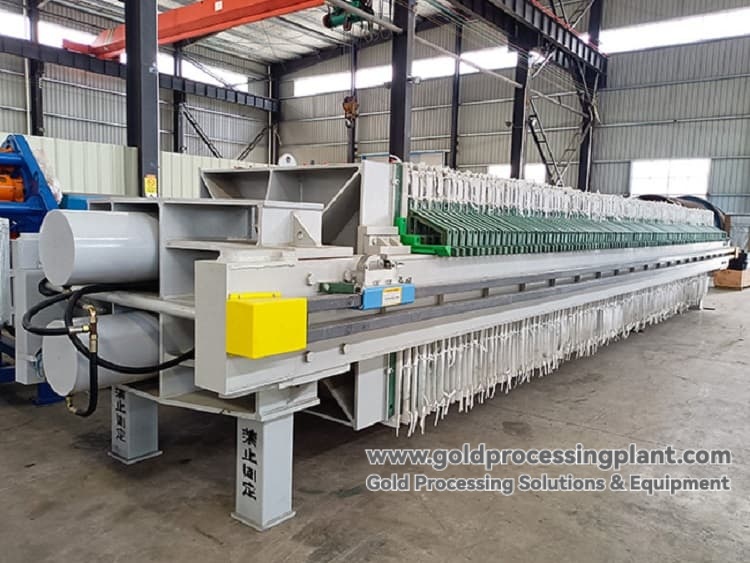
Concentration and Dewatering Section: Thickener (for dewatering slurry prior to leaching and dewatering tailings) + filter press (for dry tailings discharge) + dewatering screen.
Tailings Detoxification Section: Cyanide-containing tailings undergo detoxification treatment, such as alkaline chlorination, and are discharged or reused after meeting regulatory standards; the tailings dry stacking area is equipped with a bottom impermeable liner, drainage systems, and leachate collection.
Auxiliary Equipment: Vibrating feeder, belt conveyor, mixing tank, slurry pump, carbon recovery pump, clean water pump, recirculation pump, and electrical control system.
V. Electrolytic Leaching Solution: How to Extract Gold from Gold-Bearing Carbon
Desorption electrolysis is the “last mile” in gold recovery at a carbon-in-pulp plant. The design of this process involves several key considerations:
1. Selection of desorption method. Desorption at ambient temperature and pressure requires low investment and is simple to operate, making it suitable for small- to medium-scale operations and conventional gold-loaded carbon; high-temperature, high-pressure desorption offers high efficiency and thorough desorption, making it suitable for large-scale mines and carbon with high gold content that is difficult to desorb. When making a selection, the overall economic viability—including desorption cycle time, chemical consumption, and equipment investment—must be evaluated.
2. Coordination of the desorption solution with the electrolysis process. The desorption solution (gold-bearing solution) enters the electrolytic cell, where electrolysis deposits the gold onto the cathode to form gold sludge. The current density, electrode spacing, and electrolysis time in the electrolytic cell must be matched to the gold concentration in the desorption solution; incomplete electrolysis will cause gold to circulate in the lean solution, reducing the recovery rate.
3. Acid washing and carbon regeneration. Gold-loaded carbon must be acid-washed prior to desorption to remove carbonates and impurities. After desorption, the depleted carbon is regenerated and returned to the adsorption system for reuse. The quality of carbon regeneration directly affects the adsorption capacity of activated carbon and carbon consumption; therefore, the regeneration step cannot be omitted.
4. Gold Sludge Smelting. The gold sludge obtained from electrolysis is acid-washed and dried before being fed into a gold smelting furnace to produce refined gold. Smelting temperature and flux composition affect the purity of the gold ingots and the smelting recovery rate.
5. Automated Control. It is recommended that the desorption and electrolysis system be equipped with monitoring and control systems for temperature, pressure, flow rate, and current to ensure stable desorption rates and electrolysis efficiency. Safety interlock protection for high-temperature, high-pressure equipment must be fully implemented.
VI. Implementation of the Plan: Conduct Trials First, Then Discuss Equipment
The complexity of high-carbon gold ore means that the plan cannot be decided on a whim. GoldProcessingPlant\'s collaborative process emphasizes “understanding the ore first, then selecting equipment”:
Step 1: Mineral Processing Testing and Process Validation. Conduct chemical analysis and processability tests on representative ore samples, covering flotation tests, comparative tests of different pretreatment methods (chlorination/oxidation/roasting/biological oxidation), cyanide leaching tests, and CIP/CIL comparison tests.The test report not only provides recommended processes and expected recovery rates but also directly includes a list of equipment selections and a preliminary budget. Standard validation takes approximately 3–4 weeks, and a complete proposal report is typically issued within 30–45 days; if the ore properties are particularly complex, additional validation steps may be required, extending the timeline accordingly.
Step 2: Process Design, Equipment Selection, and Quotation. Based on the test data, the process route and parameters for pretreatment plus CIP/CIL are determined, and a process flow diagram, equipment configuration list, equipment selection plan, and budget quotation are provided.
Step 3: Engineering Drawings and Equipment Manufacturing. We provide site layout plans, equipment foundation drawings, layout diagrams, piping diagrams, and civil engineering requirement drawings. Core equipment is manufactured according to the drawings, and non-standard components are custom-made as needed.
Step 4: Installation, Commissioning, and Personnel Training. We will dispatch engineers to provide on-site installation guidance, lead the commissioning of individual units and integrated trial runs with feed material, and optimize the pre-treatment chemical regimen, grinding fineness, and leaching parameters until qualified gold is produced; we will also provide theoretical and hands-on training to the client\'s team to ensure they can independently adjust the chemical regimen, grinding fineness, and leaching parameters.
Regarding Performance Commitments: Recovery rates are determined by the inherent characteristics of the ore (grain size distribution, association with other minerals, occurrence conditions, and type of carbonaceous material); we do not commit to absolute figures that are detached from reality.What we can commit to is: through rigorous process design, we will develop a process capable of achieving the highest attainable recovery rate under the specific conditions of this ore, and we will strive for excellence in equipment selection and process control. Both parties will agree in the contract on reasonable acceptance criteria based on the same ore source and the same operating conditions.
VII. Flexible Services and Project Timeline
GoldProcessingPlant does not require bundled services and offers flexible, phased services: clients may opt for mineral processing tests only (to first assess the feasibility and economic viability of pre-treatment),obtain only a quote for process design and equipment selection, purchase only engineering drawings, procure individual units or complete sets of equipment, or engage engineers for on-site commissioning; alternatively, clients may opt for a turnkey EPC solution, which comprehensively manages design, equipment, installation guidance, and commissioning training, and assumes responsibility for the final production targets.The mineral processing test and design fees paid in the initial phase can be fully offset against the equipment cost when a subsequent equipment or EPC contract is signed.
Regarding the project timeline, the overall duration from the start of process design to final production commencement is typically between 8 and 15 months.Key milestones: Process design and equipment selection quotation (7–15 days) → Engineering drawing design (20–30 days) → Equipment manufacturing (60–120 days) → Logistics (30–60 days) → Installation and commissioning (60–150 days).The commissioning period for combined processes—including pre-treatment, CIP/CIL, and stripping electrolysis—is relatively long, so a sufficient commissioning period must be allocated; for overseas projects, additional buffer time must be set aside for customs clearance (approximately 30 days) and a transition period (approximately 30 days).
The core logic behind constructing a carbon-in-pulp (CIP) processing plant for high-carbon gold ore is clear: First, conduct mineral processing tests to identify the type of carbonaceous material and its gold-trapping capacity, and select the appropriate pretreatment path to eliminate interfering factors before leaching; then, based on leaching characteristics, choose either CIP or CIL to reliably recover the dissolved gold;equipment is selected based on process requirements, and materials are upgraded according to operating conditions; gold-bearing carbon is subjected to desorption, electrolysis, and smelting to produce high-purity gold; and tailings are detoxified and disposed of via dry discharge in compliance with regulations. With data supporting every step, recovery rates are guaranteed.